Your tinplate coil meets every thickness and surface specification. Yet it still cracks during pressing, bending, or drawing. This frustrates production teams and delays shipments.
Cracking rarely stems from one factor alone. Material properties, tooling conditions, and forming parameters interact in complex ways. You need a structured method to identify the real culprit behind each tinplate crack during can forming.
The stakes are high: scrap piles grow, tooling suffers damage, and customers file complaints. Without a systematic classification approach, you chase symptoms instead of solving root causes. This guide gives you that framework—turning random observations into actionable decisions that protect your production line.

Key Takeaways
- The crack location tells you which stress caused it, so always check the position first.
- Seven common causes include hard temper, wrong thickness, poor properties, surface defects, storage aging, tooling issues, and process problems.
- Match tinplate temper and thickness to your forming operation to prevent cracking.
- Use systematic comparison between cracking and good coils to identify the real cause.
- Inspect tooling and lubrication regularly; worn dies or poor lubrication cause cracks.
- Implement incoming tests like tensile, hardness, and bend tests to catch issues early.
- Ask your supplier for mechanical property ranges and certificates to ensure consistency.
- Distinguish between material and process problems using a diagnostic guide and comparison.
Where Does Tinplate Crack During Can Forming Occur?
Before you investigate causes, you must first identify where the crack appears. The location gives you the first clue about which factors deserve attention. Different areas of a can experience different stress patterns during forming. A crack on the side wall tells a different story than one at the bottom corner.
Cracks on the Can Body
Side Wall Cracks
Side wall cracks run vertically along the cylindrical body of the can. You typically see them during drawing or ironing operations. These cracks often indicate that the material cannot handle the tensile stress pulling it around the die. The side wall stretches the most during forming, so any weakness in the tinplate becomes visible here first.
Flange and Seam Area Cracks
Flange cracks appear at the curled edge where the can body meets the end. Seam area cracks occur near the welded or soldered joint in three-piece cans. These locations experience bending stress combined with material thinning. You should check both the material properties and the tooling geometry when cracks appear in these zones.
Cracks on Can Ends and Easy-Open Ends
Score Line and Curling Area Cracks
Easy-open ends have a score line that weakens the metal intentionally. Cracks along this line during curling indicate the scoring depth interacts poorly with the material’s formability. The curling operation bends the metal around a tight radius, and any pre-existing stress concentration at the score line can propagate into a visible crack.
Pressed Section and Tab Area Cracks
The pressed section where the tab attaches undergoes complex deformation. Material flows in multiple directions simultaneously. Cracks here often point to insufficient formability for the specific geometry you are forming. The tab area also experiences repeated stress during opening, so any micro-crack from forming can grow during use.
Cracks in Deep-Drawing and Bending Areas
Bottom Corner and Transition Area Cracks
Deep-drawing operations place the most severe stress at the bottom corner. This transition zone between the flat bottom and the vertical wall experiences extreme thinning. The material must flow around a small radius while being pulled in two directions. Cracks here frequently indicate that the drawing ratio exceeds what the material can accommodate.
Longitudinal Bending and Flanging Cracks
Three-piece cans undergo longitudinal bending when the flat sheet forms into a cylinder. Flanging then curls the edges outward. These operations create bending stress along the grain direction of the steel. If the material’s directionality differs from the bending axis, you may see cracks along the bend line.
| Crack Location | Possible Cause |
|---|---|
| Side wall | Excessive tensile stress during drawing |
| Flange | Tooling geometry or material formability |
| Seam area | Welding-related stress or forming strain |
| Bottom corner | Drawing ratio exceeds material capacity |
| Score line | Score depth interacts with material properties |
| Bend area | Material directionality or excessive strain |
This table serves as a starting point for your troubleshooting, not a definitive diagnosis. Each location can have multiple contributing factors. You must examine the specific conditions of your operation to determine which cause applies. The next section explores the seven most common causes of tinplate crack during can forming in detail.
The 7 Most Common Causes of Tinplate Cracking
You now know where cracks appear on your cans. The next step is understanding why they form. Seven factors account for nearly every tinplate crack during can forming you will encounter on your production line. Each one interacts with the others, so you must examine them together rather than in isolation.
1. Tinplate Temper Is Too Hard for the Forming Operation
Temper controls the balance between strength and formability in your tinplate. When you select a temper that is too hard for your specific forming operation, the material cannot deform enough to follow your tooling geometry. The forming force increases, local stress concentrates at critical points, and the metal fractures before reaching its final shape.
The temper designation system runs from T1 through T5 for single-reduced material and DR7 through DR9 for double-reduced grades. The table below shows how mechanical properties change across this range.
| Temper (ASTM/JIS) | Yield Strength (MPa) | Tensile Strength (MPa) |
|---|---|---|
| T1 | 230 | 325 |
| T2 | 245 | 340 |
| T3 | 275 | 375 |
| T4 | 290 | 390 |
| T5 | 435 | 460 |
| DR7M/DR7.5 | 520 | 545 |
| DR8 | 550 | 575 |
| DR9 | 620 | 625 |
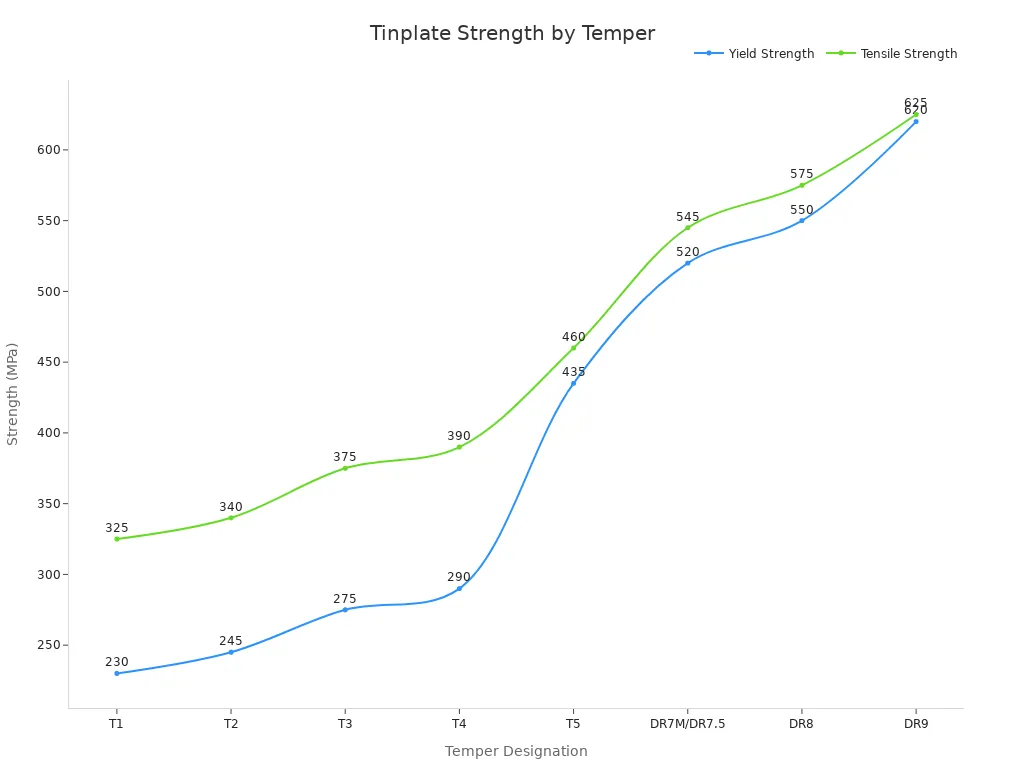
This data reveals a clear trend. As the temper designation increases, both yield and tensile strength rise significantly. Higher strength means lower ductility, which directly reduces formability and increases cracking tendency.
For shallow to medium draws, single-reduced tempers T3–T4 work well. They minimize wrinkling while preserving panel strength. For very lightweight bodies, double-reduced tempers DR8–DR9 allow thinner gauges while maintaining buckle strength. However, these harder tempers demand sharper tool maintenance and tighter lubrication control. You cannot run them with worn dies or inconsistent lubricant application.
Double-reduced tempers such as DR8–DR10 offer stiffness at low gauge, but they require precise score depth control, especially for can ends. A small variation in scoring pressure can trigger a crack that would not appear with softer material.
You should not assume that one temper works for every application. The correct choice depends on your can design, forming depth, geometry, thickness, and production process. Consult the tinplate temper chart to understand the full range of options before making your selection.
2. Thickness Is Not Suitable for the Can Design
Many production managers assume that thinner tinplate always causes cracking. This oversimplification leads you in the wrong direction. The real question is whether your thickness suits your forming design and process.
Too-thin material leaves less forming margin. The metal thins further during drawing, and you have less reserve to absorb local stress variations. Too-thick material increases the forming force required. Your press must work harder, and the additional force can create stress concentrations at corners and transitions.
Thickness variation within a coil also creates inconsistent forming behavior. One section may form perfectly while another cracks, even though both come from the same coil. This inconsistency frustrates operators and makes troubleshooting difficult.
You must evaluate thickness against your specific forming geometry. A deep-drawn can with sharp bottom corners needs different thickness than a shallow drawn container with generous radii. Review the tinplate thickness guide to understand how thickness interacts with your forming requirements.
3. Mechanical Properties Are Outside the Required Range
Two tinplate coils with the same nominal thickness can behave completely differently during forming. This happens when their mechanical properties differ. Yield strength, tensile strength, elongation, and hardness all affect how the material responds to deformation.
Yield strength tells you when the material starts to deform permanently. Higher yield strength means you need more force to shape the metal. Tensile strength indicates the maximum stress the material can withstand before fracture. Elongation measures how much the material can stretch before breaking. Lower elongation means less deformation capacity and higher cracking risk.
You cannot rely on thickness alone when evaluating tinplate for your process. A coil that meets thickness specifications may still fail if its yield strength runs higher than your forming equipment can handle. This situation occurs more often than you might expect, especially when you switch suppliers or receive material from different production batches.
For procurement managers, this point matters greatly. You must specify mechanical property ranges, not just thickness and temper designations. Ask your supplier for the tensile and yield strength values on every certificate of analysis. Compare these numbers against the coils that performed well in your production line. This comparison gives you a reliable baseline for future orders.
The interaction between mechanical properties and your forming process determines whether you see a tinplate crack during can forming. A material with borderline elongation may work fine at low forming speeds but crack when you increase production rates. The same material may also fail when your tooling wears beyond a certain point.
You should also consider material direction. Rolling direction affects formability in bending and drawing operations. The material behaves differently along the rolling direction compared to the transverse direction. Your blank orientation must account for this difference, especially for deep-drawn parts with complex geometry.
Tooling problems can also produce cracks that look like material defects. Die radius, alignment, clearance, and wear all influence forming results. Not every crack is a material defect. You must inspect your tooling before blaming the tinplate.
Could Surface Defects or Tin Coating Cause Cracking?
You inspect a coil and spot scratches or pits on the surface. Your first instinct says these defects caused the crack. The truth is more complex. Surface defects can contribute to cracking, but they rarely act alone. You must understand how they interact with your forming process before you assign blame.
Surface Defects as Stress Concentration Points
Surface defects include scratches, pits, roll marks, edge defects, and burrs. These imperfections interrupt the smooth flow of metal during forming. When the material stretches around a die, the defect creates a local area where stress concentrates. This concentration can exceed the material’s strength and initiate a crack.
However, a surface defect does not automatically mean your tinplate will crack. The outcome depends on several factors working together. Defect depth matters most. A shallow scratch may stretch harmlessly during forming. A deep pit penetrates further into the steel substrate and creates a more severe stress concentration.
Location also plays a critical role. A defect on a flat panel area experiences less stress than one at a bend radius or a deep-drawn corner. The same scratch that causes no problem on the side wall may trigger a crack at the bottom corner where material thinning is extreme.
Your forming severity determines whether a defect becomes critical. Light bending operations may tolerate minor surface imperfections. Deep drawing with high reduction ratios leaves no margin for error. The material already operates near its forming limit, so any additional stress concentration pushes it over the edge.
Material properties influence the outcome as well. A softer temper with higher elongation can absorb more local stress before fracturing. A harder temper with lower ductility has less capacity to accommodate the same defect. You must evaluate surface quality together with your material specification and forming conditions.
You should document any surface defects you find during incoming inspection. Use the tinplate quality inspection checklist to record defect type, location, and severity. This documentation helps you correlate defects with cracking patterns later. Without this record, you cannot determine whether the defect caused the problem or appeared coincidentally.
The Role of Tin Coating and Surface Treatment
When the steel substrate cracks, you might wonder if the tin coating contributed. In most cases, the coating is not the first factor you should investigate. The steel base material carries the structural load during forming. The tin layer provides corrosion resistance and solderability, not mechanical strength.
Tin coating thickness typically ranges from 0.1 μm to 1.5 μm per side depending on your application. This layer is extremely thin compared to the steel substrate. It cannot prevent or cause a crack in the underlying metal. You should focus your investigation on substrate properties, tooling conditions, and forming parameters first.
That said, coating uniformity and surface treatment can play a secondary role. Uneven coating creates areas with different friction characteristics. These variations affect material flow during forming and may contribute to localized stress. Passivation layers and oil films also influence friction and wear behavior.
You should examine the coating when you see surface-related cracking patterns. Check for bare spots, excessive roughness, or inconsistent passivation. These conditions can alter how the material interacts with your tooling. Review the tinplate coating weight guide to understand what specifications apply to your process.
The practical approach is simple. Rule out substrate, tooling, and process factors first. If those check out and surface-related cracking persists, then examine coating uniformity and surface treatment. This systematic method prevents you from chasing the wrong variable and wasting production time.
Does Storage or Aging Affect Tinplate Formability?
You receive a coil, store it for several weeks, then run it through your press. Cracks appear that you never saw before. Your first instinct blames the supplier. Before you make that call, consider what happened inside your warehouse. Storage conditions and aging can change how tinplate behaves during forming.
The Impact of Storage Conditions and Aging
Tinplate does not remain perfectly static after production. The steel substrate and its surface treatment respond to their environment over time. Temperature swings, humidity levels, and storage duration all influence the material’s condition.
High humidity creates the most visible problem: rust. Surface oxidation weakens the protective tin layer and creates rough spots. These areas increase friction during forming. Higher friction means more heat and more force at the die interface. The material stretches unevenly, and cracks appear where you least expect them.
Temperature fluctuations cause condensation. Moisture forms on the coil surface when warm air meets cold metal. This moisture accelerates corrosion and can degrade the oil film applied at the mill. That oil film controls friction during your forming operation. Once it breaks down, the material behaves differently against your tooling.
Long storage periods also allow the steel to age naturally. Strain aging occurs when carbon and nitrogen atoms migrate to dislocations within the crystal structure. This movement increases yield strength and reduces ductility over time. A coil that formed perfectly when fresh may crack after months in storage because the material has become harder and less forgiving.
The surface condition changes too. Passivation layers can degrade, exposing the tin coating to environmental attack. The protective oil film evaporates or collects dust. These changes alter the friction characteristics you relied on during your initial process setup.
Separating Storage Issues from Intrinsic Material Defects
You must distinguish between a coil that arrived defective and one that deteriorated in your warehouse. This distinction determines who bears responsibility and what corrective action you take.
Start by checking your receiving records. Did the coil pass incoming inspection when it arrived? If yes, the material met your specifications at delivery. Any subsequent change points to storage conditions or handling practices.
Compare fresh coils against stored coils from the same production batch. Run both through your forming line under identical conditions. If fresh material forms without cracks but stored material fails, your storage environment deserves scrutiny. The supplier did not send you defective tinplate.
A coil that forms perfectly upon arrival and cracks after three months of storage is a storage problem, not a supplier problem.
You should also examine your storage practices. Are coils stored upright on their edges? Is the warehouse climate-controlled? Do you rotate stock using a first-in, first-out system? Each of these factors affects how long tinplate remains in optimal forming condition.
When cracking increases after storage, investigate three areas together: the material’s original specification, your storage environment, and the surface condition at the time of forming. Do not isolate one variable. The interaction between these factors determines whether your tinplate cracks during can forming.
Document everything. Record storage duration, temperature readings, humidity levels, and the date each coil entered your warehouse. This data helps you correlate storage conditions with forming performance. Without this record, you cannot prove whether the material degraded or arrived defective.
How to Troubleshoot Tinplate Crack During Can Forming
You now have a clear picture of where cracks appear and what causes them. The next challenge is turning that knowledge into a practical response. This section gives you a five-step checklist you can apply the moment you spot a crack on your production line. Follow these steps in order. Each one narrows your investigation and brings you closer to the root cause.
Step 1: Identify the Crack Location
Record the exact position of every crack you observe. Note whether it appears on the can body, flange, bottom corner, seam, end, or score line. Take photographs and mark the location on a sample can. This record becomes your reference point for all subsequent analysis.
The location tells you which stresses acted on the material. A crack at the bottom corner points to drawing stress. A crack along the score line suggests scoring depth issues. A crack at the flange indicates bending or curling problems. Write down the orientation of the crack as well. Vertical cracks differ from horizontal ones in what they reveal about material flow.
You should also note whether the crack appears at the start, middle, or end of a production run. This timing information helps you determine whether tooling wear or material variation plays a role.
Step 2: Check if Cracking Is Coil-Specific or Widespread
Determine whether the problem affects one coil or multiple coils. This single observation dramatically narrows your investigation.
If only one coil shows cracking, the issue likely stems from material variation within that specific coil. Check the coil’s production date, supplier, and incoming inspection records. Compare these against coils that formed without problems.
If multiple coils crack, the issue likely involves your process or tooling. A change in die alignment, forming speed, or lubrication affects every coil you run. The material may be fine, but your process conditions have shifted.
You should also check whether the cracking pattern follows a coil position. Cracks near the coil edges suggest edge effects from slitting. Cracks in the middle indicate core material properties. This positional information adds another layer to your diagnosis.
Step 3: Review Tinplate Specification and Mechanical Properties
Pull the specification for the cracking coil and compare it against your requirements. Check thickness, temper, mechanical properties, tin coating, surface condition, and width. Each parameter must fall within the agreed range.
Thickness affects hardness testing results. Very thin sheets below 0.20 mm require a different Rockwell scale, the 15T scale, to avoid anvil effects that distort readings. If you test hardness on thin material with the wrong scale, you get misleading numbers that send you in the wrong direction.
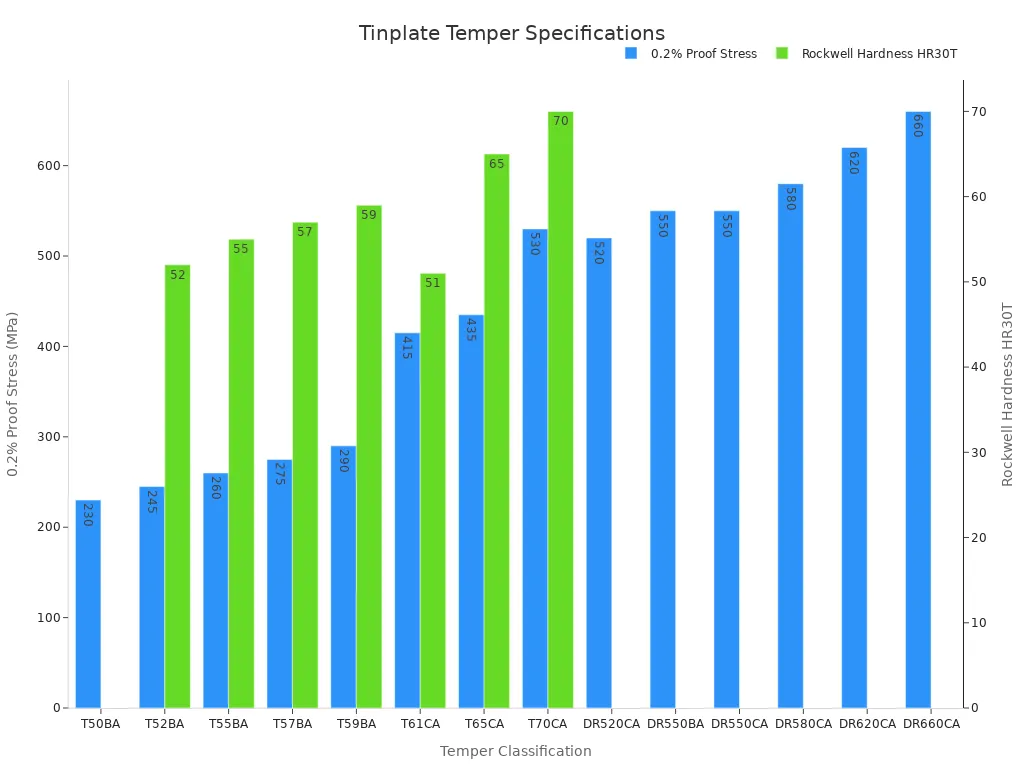
For single-reduced tinplate, the Rockwell superficial hardness test on the R30T scale determines the temper designation. Temper grades like T52BA or T55BA correspond to specific target HR30T values. Measure the hardness of your cracking coil and compare it against the specified temper range.
For double-reduced tinplate, tensile properties matter more than hardness. The 0.2% proof stress values, such as 230 MPa or 245 MPa, define each temper grade. You should also run the springback test, which serves as a routine method to determine proof stress for double-reduced material. This test gives you a practical measure of how the material will behave during forming.
Compare your measured values against the certificate of analysis from the supplier. If the numbers match, the material meets specification. If they differ, you have found a material-related cause for your tinplate crack during can forming.
Step 4: Inspect Forming Conditions and Tooling
Examine your die radius, forming speed, pressure, clearance, drawing ratio, and lubrication. Each parameter affects how the material flows during forming. A die radius that worked for a softer temper may crack a harder one. A clearance that suits one thickness may fail with another.
Check your tooling for wear, alignment, and surface condition. Worn dies create uneven stress distribution. Misaligned tools cause asymmetric loading. Burrs or sharp edges on the tooling scratch the material surface and create stress concentration points.
Verify your lubrication system delivers consistent coverage. Insufficient lubricant increases friction and local heating. Excess lubricant can cause slippage and inconsistent forming. Measure the lubricant application rate and confirm it matches your process specification.
Step 5: Compare With a Previously Successful Coil
The most practical quality control approach involves direct comparison. Take a coil that formed without cracks and compare it against the cracking coil. Examine thickness, hardness, tensile strength, yield strength, elongation, temper, surface condition, supplier, and production date.
This comparison reveals subtle differences that specifications may miss. Two coils can both meet the same specification range yet sit at opposite ends of that range. A coil at the high end of yield strength may crack while one at the low end forms perfectly.
Document these comparisons for every coil you receive. Build a database of successful coils and their properties. Over time, this database tells you which property ranges work reliably for your specific forming operations. You can then tighten your incoming inspection criteria to match what actually performs well on your line.
This systematic approach transforms troubleshooting from guesswork into a structured process. You identify the real cause, implement the right fix, and prevent future occurrences.
How to Prevent Tinplate Cracking in Your Process
Prevention beats troubleshooting every time. You can eliminate most cracking issues before they reach your production line by making deliberate choices at three control points: material selection, tooling maintenance, and incoming inspection. Each control point gives you a chance to catch problems early and protect your forming operation.
Match Temper and Thickness to Forming Requirements
Your first line of defense starts with the material specification. You must match temper and thickness to the actual demands of your can design. A deep-drawn container with tight radii needs a softer temper that can flow into complex shapes without fracturing. A flat lid or shallow panel needs a harder temper to resist buckling and maintain panel strength.
| Selection Parameter | Key Data Points | Direct Application to Prevent Cracking |
|---|---|---|
| Temper Grade (Hardness) | T1 (HR30T 46-52) – softest, for deep drawing; T2 (50-56) – general food cans; T3 (54-60) – lids/shallow; T4 (58-64) – ends/closures; T5 (62-68) – flat parts, high strength; DR7M-DR10 (68-85) – ultra-thin, high strength | For complex, deep-drawn can shapes with tight radii, select T1 or T2 (softer) to allow material flow without fracture. For flat lids or shallow, rigid panels, select T4 or T5 (harder) to resist buckling. DR grades provide high strength at reduced thickness, useful for lightweight designs where cracking from thinning must be avoided. |
| Thickness (Base Weight) | 60 lb (0.0066 in / 0.168 mm); 70 lb (0.0075 in / 0.190 mm); 80 lb (0.0082 in / 0.208 mm); 90 lb (0.0093 in / 0.236 mm); 100 lb (0.0104 in / 0.264 mm) | Thicker material (90-100 lb) provides more metal for severe forming, reducing risk of localized thinning and cracking. Thinner material (60-70 lb) suits shallow draws but requires a harder temper to maintain strength. Use the chart to match base weight to required thickness, ensuring the chosen gauge can withstand the forming strain without rupture. |
| Supplier Confirmation | Always confirm temper grade with supplier before production | This step verifies that the actual delivered material’s hardness matches the design assumption, preventing unexpected cracking due to off-specification temper. |
You should also define mechanical property requirements beyond just temper designation. Specify yield strength, tensile strength, and elongation ranges in your purchase order. This practice ensures every coil you receive behaves consistently during forming. Two coils with the same temper grade can still differ in mechanical properties if they come from different production batches.
Control Tooling and Lubrication
Your tooling condition directly affects whether the material cracks. A die radius that worked for a softer temper may fail with a harder one. Worn tooling creates uneven stress distribution that concentrates at critical points. Misaligned dies cause asymmetric loading that pulls the material unevenly.
Inspect your tooling regularly. Check die radius, alignment, clearance, and surface condition before each production run. Replace worn tools before they cause problems. A small investment in tooling maintenance prevents costly scrap and downtime.
Lubrication deserves equal attention. Insufficient lubricant increases friction and local heating at the die interface. This heat raises the forming force and creates localized stress that can initiate cracks. Excess lubricant causes slippage and inconsistent material flow.
Verify your lubrication system delivers consistent coverage across the entire forming area. Measure the application rate and confirm it matches your process specification. Check that the lubricant type suits your material and forming operation. Different tempers and thicknesses may require different lubrication strategies.
Implement Incoming Material Inspection
You cannot prevent what you do not measure. A robust incoming inspection program catches material problems before they reach your press. This program protects your production line and gives you documented evidence when you need to discuss issues with your supplier.
Your inspection should include several key tests that directly relate to cracking resistance:
- Tensile test: Assesses mechanical strength and ductility, directly related to cracking resistance under stress.
- Rockwell hardness test: Measures surface hardness, which influences crack initiation and propagation.
- Springback test: Evaluates elastic recovery, indicating formability and potential for cracking during forming.
- Bend tests and cupping tests: Assess formability and surface ductility, critical for detecting susceptibility to cracking during stamping or drawing.
- Tin crystal size (TCS) test: Uses ASTM E112 grain size charts to predict tinplate performance, as grain size affects mechanical integrity and crack resistance.
Record every test result and compare it against your specification. Build a database of coil performance over time. This data tells you which property ranges work reliably for your specific forming operations. You can then tighten your acceptance criteria to match what actually performs well on your line.
A coil that passes inspection but cracks during forming is a process problem. A coil that fails inspection and cracks during forming is a material problem. The distinction determines your corrective action.
Document the supplier, production date, and test results for every coil you receive. This record helps you identify trends and correlate material properties with forming performance. When you spot a pattern, you can address it before it becomes a production issue.
What Should Can Makers Ask Their Tinplate Supplier?
Your supplier holds the answers to most cracking problems. You just need to ask the right questions. A structured conversation about material specification prevents surprises on your production line. The questions below give you a framework for that conversation.
Key Questions on Material Specification and Quality
Start with the basics. Ask what temper grade your supplier ships. The temper designation tells you the balance between strength and formability. Single-reduced grades like T52BA through T59BA suit drawing and general forming. Double-reduced grades such as DR550CA or DR620CA provide higher strength for ends and bodies. Your forming operation determines which range you need.
| Temper Grade | 0.2% Proof Stress (MPa, ±50) | Rockwell Hardness HR30T (±4) | Typical Use |
|---|---|---|---|
| T52BA | 245 | 52 | Drawing |
| T55BA | 260 | 55 | General purpose, aerosol tops |
| T57BA | 275 | 57 | General purpose, aerosol bodies |
| T59BA | 290 | 59 | General purpose |
| DR550CA | 550 | – | Ends and bodies |
| DR620CA | 620 | – | Ends and DRD cans |
Ask about mechanical property ranges, not just temper names. Request the tensile strength, yield strength, and elongation values for each coil. Two coils with the same temper grade can behave differently if their properties sit at opposite ends of the tolerance band. A coil at the high end of yield strength may crack where one at the low end forms perfectly.
Thickness tolerance matters just as much. Tinplate substrate ranges from 0.10 mm to 0.49 mm, with the tin coating adding 0.1 μm to 1.5 μm per side. Ask your supplier what tolerance they hold. A tight tolerance means consistent forming behavior. A loose tolerance creates variation that shows up as intermittent cracking.
Surface finish and tin coating weight complete the picture. Ask what surface finish your supplier provides and whether differential coating is available. The steel substrate should maintain a roughness of Ra ≤1.5 μm to ensure uniform tin plating adhesion. The elastic modulus typically runs 200-210 GPa, dominated by the steel substrate.
Requesting Documentation and Samples for Testing
A verbal promise means nothing without documentation. Request a Mill Test Certificate (MTC) or Certificate of Analysis (COA) for every coil you order. This document records the chemical composition, mechanical properties, and heat treatment of the material.
| MTC Field | What It Means | How to Interpret It |
|---|---|---|
| Heat No: X-12345 | Unique identifier for the production batch | Match this number to the physical material markings |
| Tensile Strength: 590 MPa | Maximum stress before fracture | Verify it meets your minimum requirement |
| Yield Strength: 280 MPa | Point of permanent deformation | Ensure it falls within your acceptable range |
| Elongation: 45% | How much the material stretches before breaking | Higher percentage means greater ductility |
Verify the certificate properly. Match the heat number on the MTC to the markings on the coil. Confirm the product description and grade match your purchase order. Review the chemical composition and mechanical property results against your specification. Check that the certificate is original, not photocopied or altered.
Ask for production samples before committing to a large order. Run those samples through your actual forming line under production conditions. This test reveals how the material behaves with your tooling, lubrication, and forming speed. A sample that forms without cracks gives you confidence. One that cracks saves you from a costly mistake.
Ask whether your supplier can maintain consistent mechanical properties between coils. This question matters more than any other. Consistency between batches determines whether your process runs smoothly or requires constant adjustment. A supplier who controls their process tightly delivers coils that behave the same way every time.
When Is Tinplate the Problem—and When Is It the Process?
You face a crack on your line and need a fast answer. Is the coil defective, or did your process change? The distinction determines your next move. Blaming the material when the process shifted wastes time and money. Adjusting the process when the material drifted creates more scrap. You need a reliable way to separate these two scenarios.
A Diagnostic Guide Based on Observations
Your observations on the production floor provide the first clues. Certain patterns point clearly toward material issues. Others indicate process problems. The table below maps common observations to the first area you should investigate.
| Observation | First Area to Investigate |
|---|---|
| Cracks only after a tooling change | Tooling |
| Cracks across multiple suppliers | Process |
| Cracks only on one coil | Material |
| Cracks at the same location every time | Tool / geometry |
| Cracks increase with higher forming speed | Process |
| Cracks appear after long storage | Storage + material |
| Hardness differs from previous coil | Material |
Consider the base steel type in your diagnosis. Single-reduced (SR) steel suits deep drawing operations. Double-reduced (DR) steel provides stiffness at lower thickness. If you run a deep draw with DR material, you selected the wrong steel. That is a material selection error, not a process fault.
Temper grades from T2 through T4 and DR8 through DR10 each serve different purposes. You can verify the temper using strip tension curves. Pilot forming trials reveal whether springback comes from a temper mismatch or from tooling pressure. Run a small batch with known-good material. If the trial forms cleanly, your process works. The problem lies in the coil.
Thickness tolerances also offer diagnostic value. Run seamer stack-up and buckle tests at the minimum thickness tolerance. If failures occur only at that minimum, you face process tolerance drift, not a material defect. The coil meets specification. Your process cannot handle the variation within that specification.
Surface finish and tin coating thickness complete the picture. Stone, bright, and matte finishes each align with different friction and ink adhesion targets. If friction issues persist across all finishes, your lubrication system needs attention. Tin coating thicknesses range from 0.1 μm to 1.5 μm per side. Solderability or retort failures that appear only in one coil point to a material batch issue, not your line settings.
The Importance of Systematic Comparison
A single observation rarely tells the whole story. You need a systematic comparison between the cracking coil and a known-good coil. This approach delivers more reliable answers than immediately changing the material.
Start with the certificate of analysis from both coils. Compare thickness, hardness, tensile strength, yield strength, and elongation values. Two coils can both meet specification yet sit at opposite ends of the tolerance band. A coil at the high end of yield strength may crack where one at the low end forms perfectly.
Check the production dates and suppliers. A coil from a different production batch may behave differently even with identical specifications. Record every comparison in a database. Over time, this database reveals which property ranges work reliably for your specific forming operations.
A systematic comparison between the cracking coil and a known-good coil delivers more reliable answers than immediately changing the material.
This method transforms your response to any tinplate crack during can forming. You stop guessing and start measuring. You identify the real variable that changed. Then you fix that variable with confidence.
The diagnostic table gives you a starting point. The systematic comparison confirms your diagnosis. Together, they protect your production line from both material defects and process drift. You gain control over your forming operation and reduce scrap before it grows.
Tinplate cracking rarely traces to one variable. You face a material–process interaction that demands a structured response. The five-factor framework guides your investigation: Material → Specification → Tooling → Forming → Inspection. Each factor interacts with the others, so you must examine them together.
Material → Specification → Tooling → Forming → Inspection
A systematic classification approach does more than identify defects. It helps you understand your entire can forming system. You stop reacting to symptoms and start addressing root causes.
Adopt this framework proactively. Use it for continuous improvement and clearer supplier communication. You will produce higher quality cans and reduce production costs. Modern can making rewards data-driven process control. Your classification records become that data foundation.
FAQ
Why does tinplate crack when bending?
Bending creates tensile stress on the outer surface and compressive stress on the inner surface. When the material’s elongation cannot accommodate this strain, cracks appear along the bend line. Check your temper grade and the bend radius against the material’s formability limits before adjusting your process.
Does harder tinplate crack more easily?
Yes, harder tempers have lower ductility. As temper increases from T1 to DR9, yield strength rises and elongation drops. This reduced deformation capacity means less tolerance for tight radii or aggressive forming. Match your temper to the actual forming severity, not just the final strength requirement.
Can tinplate thickness variation cause cracking?
Thickness variation creates inconsistent forming behavior. Thin sections thin further during drawing, leaving less material to absorb stress. Thick sections increase forming force. Both conditions can trigger cracks. Measure thickness across the coil width and along its length to identify variation patterns.
Can scratches on tinplate cause cracks during forming?
Scratches act as stress concentration points. Whether they cause cracking depends on defect depth, location, and forming severity. A shallow scratch on a flat panel may stretch harmlessly. The same scratch at a deep-drawn corner can initiate a crack. Document defects during incoming inspection.
How can I test tinplate formability before production?
Run tensile tests to measure yield strength, tensile strength, and elongation. Perform bend tests and cupping tests to assess ductility under deformation. Compare results against coils that formed successfully. Request production samples from your supplier and run them through your actual line before committing to large orders.
Should I choose softer tinplate to prevent cracking?
Not always. Softer material forms more easily but may lack the strength your can design requires. Panel strength, buckle resistance, and dent resistance all depend on temper. Select the softest temper that still meets your final performance requirements. Test samples to confirm both formability and finished can strength.
What information should I send to a tinplate supplier when troubleshooting cracks?
Send the crack location, photographs, coil production date, and certificate of analysis. Include your forming parameters: die radius, drawing ratio, speed, and lubrication type. Compare these against a known-good coil. This information helps your supplier identify whether the issue stems from material variation or process conditions.